Infographic showing RO Plant workflow: Raw Water → Pre-treatment → Pressurization → Membrane Separation → Post-treatment → Purified Water Output
“Industrial and commercial reverse osmosis systems designed for drinking, industrial, and food processing applications.”
Reverse Osmosis (RO) is a highly effective water purification method that removes dissolved minerals, salts, and contaminants from river, sea, and groundwater. Universal Water Chemicals Pvt. Ltd. manufactures and supplies industrial RO Plants suitable for drinking water, food processing, boiler feed, pharmaceutical, and industrial applications.
Available flow rates: 100 LPH → 10,000 LPH (higher capacities custom-built)
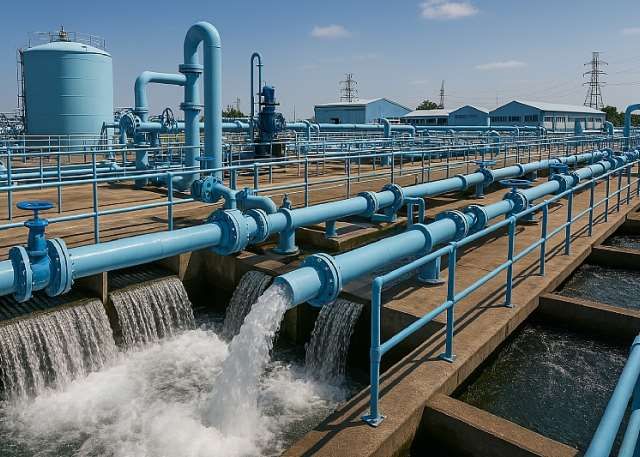
Image of installed RO plant or animation showing purified water output
The first stage of the RO process ensures that incoming water is prepared for efficient purification. Pre-treatment removes sediments, chlorine, and hardness, which protects the RO membranes from damage and scaling.
Components & Functions:
Sand & multimedia filters: Remove silt, sand, and suspended solids
Activated carbon filters: Remove chlorine, odor, and discoloration
Water softeners: Reduce hardness to prevent scaling on membranes
Benefits:
Extends membrane lifespan
Ensures smooth operation of RO plant
Improves the overall quality and taste of water
After pre-treatment, water is pumped under high pressure to pass through the RO membranes efficiently. The pressure applied depends on the TDS (Total Dissolved Solids) level in the feed water.
Components & Functions:
High-pressure pumps with energy-efficient motors
Pressure sensors to monitor and maintain optimal flow
Benefits:
Ensures maximum water recovery and purification
Reduces energy consumption by optimizing pressure
Maintains consistent flow and quality through the RO system
In this critical stage, water passes through semi-permeable RO membranes, which remove dissolved salts, minerals, heavy metals, and contaminants. Only purified water passes through, while impurities are rejected.
Components & Functions:
High-quality TFC RO membranes
Flow restrictors to maintain pressure across membranes
Reject water outlet system for safe disposal
Benefits:
Produces safe, clean water suitable for industrial, commercial, and drinking purposes
Reduces TDS to safe levels for consumption and industrial processes
Removes contaminants that can damage equipment or affect product quality
After membrane filtration, water undergoes final adjustments for safe usage. This stage includes pH balancing, mineral enhancement, and optional UV/ozone sterilization.
Components & Functions:
pH boosters (UNI Booster+, food-grade) to balance acidity
Mineral addition units for taste and nutritional quality
Optional UV sterilizers or ozone treatment for microbial safety
Benefits:
Produces water safe for drinking and industrial use
Prevents corrosion in pipes, boilers, and equipment
Ensures water meets regulatory standards and customer requirements
Water purified by RO is suitable for agriculture, industrial, and potable applications
Homes, small offices, cafes
Hotels, restaurants, medium industries
factories, hospitals, municipal supply
Prevents scale formation
Adjusts pH in product water
UNI CLEANSER I, II, III
“Contact Universal Water Chemicals for customized RO solutions for drinking,
industrial, and commercial applications.”