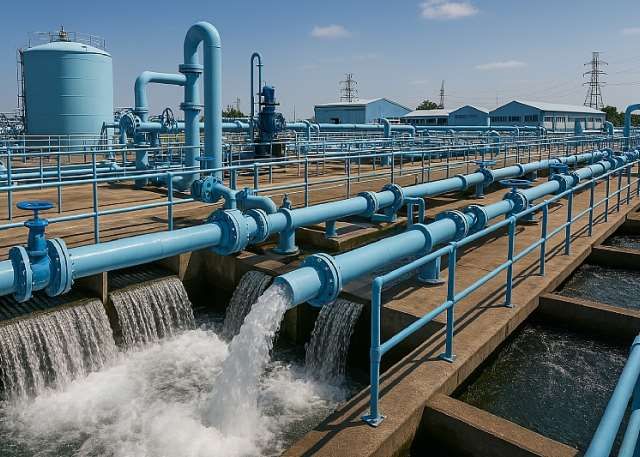
Saline/Raw Water → Pre-treatment → RO Desalination / Ion Exchange → Post-treatment → High-Purity Water Output
“Advanced Desalination and Demineralization (D.M.) Plants for industrial, commercial, and high-purity water applications.”
Desalination and Demineralization (D.M.) Plants are designed to remove dissolved salts, minerals, and impurities from water to produce high-purity water for industrial and commercial use. Universal Water Chemicals Pvt. Ltd. offers custom-built desalination and D.M. systems suitable for boiler feed, pharmaceuticals, power plants, and process industries.
The first stage prepares raw or saline water by removing suspended solids, turbidity, and contaminants, ensuring efficient downstream processing.
Components & Functions:
Sand Filters: Remove suspended particles and turbidity
Activated Carbon Filters: Remove chlorine, odor, and organic matter
Chemical Dosing Systems: Prevent scaling and fouling
Benefits:
Protects membranes and resins from damage
Improves system efficiency
Ensures consistent water quality
In desalination systems, water is passed through high-pressure RO membranes to remove dissolved salts and impurities.
Components & Functions:
High-Pressure Pumps: Force water through membranes
RO Membranes: Separate salts and contaminants
Reject System: Discharge concentrated brine
Benefits:
Converts saline water into usable water
Reduces TDS to safe levels
Suitable for industrial and potable applications
In D.M. plants, water passes through cation and anion exchange resins to remove dissolved ions completely.
Components & Functions:
Cation Resin: Removes positive ions (Ca²⁺, Mg²⁺, Na⁺)
Anion Resin: Removes negative ions (Cl⁻, SO₄²⁻)
Mixed Bed Unit (Optional): Produces ultra-pure water
Benefits:
Produces high-purity, low-conductivity water
Ideal for boilers, pharmaceuticals, and power plants
Prevents scaling and corrosion
Final stage ensures water is stabilized, stored, and ready for use.
Components & Functions:
pH Adjustment Systems: Stabilize water chemistry
Storage Tanks: Safe storage of treated water
Polishing Units: Final purification if required
Benefits:
Ensures safe and stable water quality
Ready for industrial and high-purity applications
Maintains consistent output quality
labs, small industries
commercial and mid-size industries
power plants, pharmaceuticals, large industries
prevent scaling in RO membranes
maintain ion exchange efficiency
stabilize water chemistry
ensure microbial safety
“Contact Universal Water Chemicals for customized desalination and D.M.
plant solutions for industrial and commercial applications.”